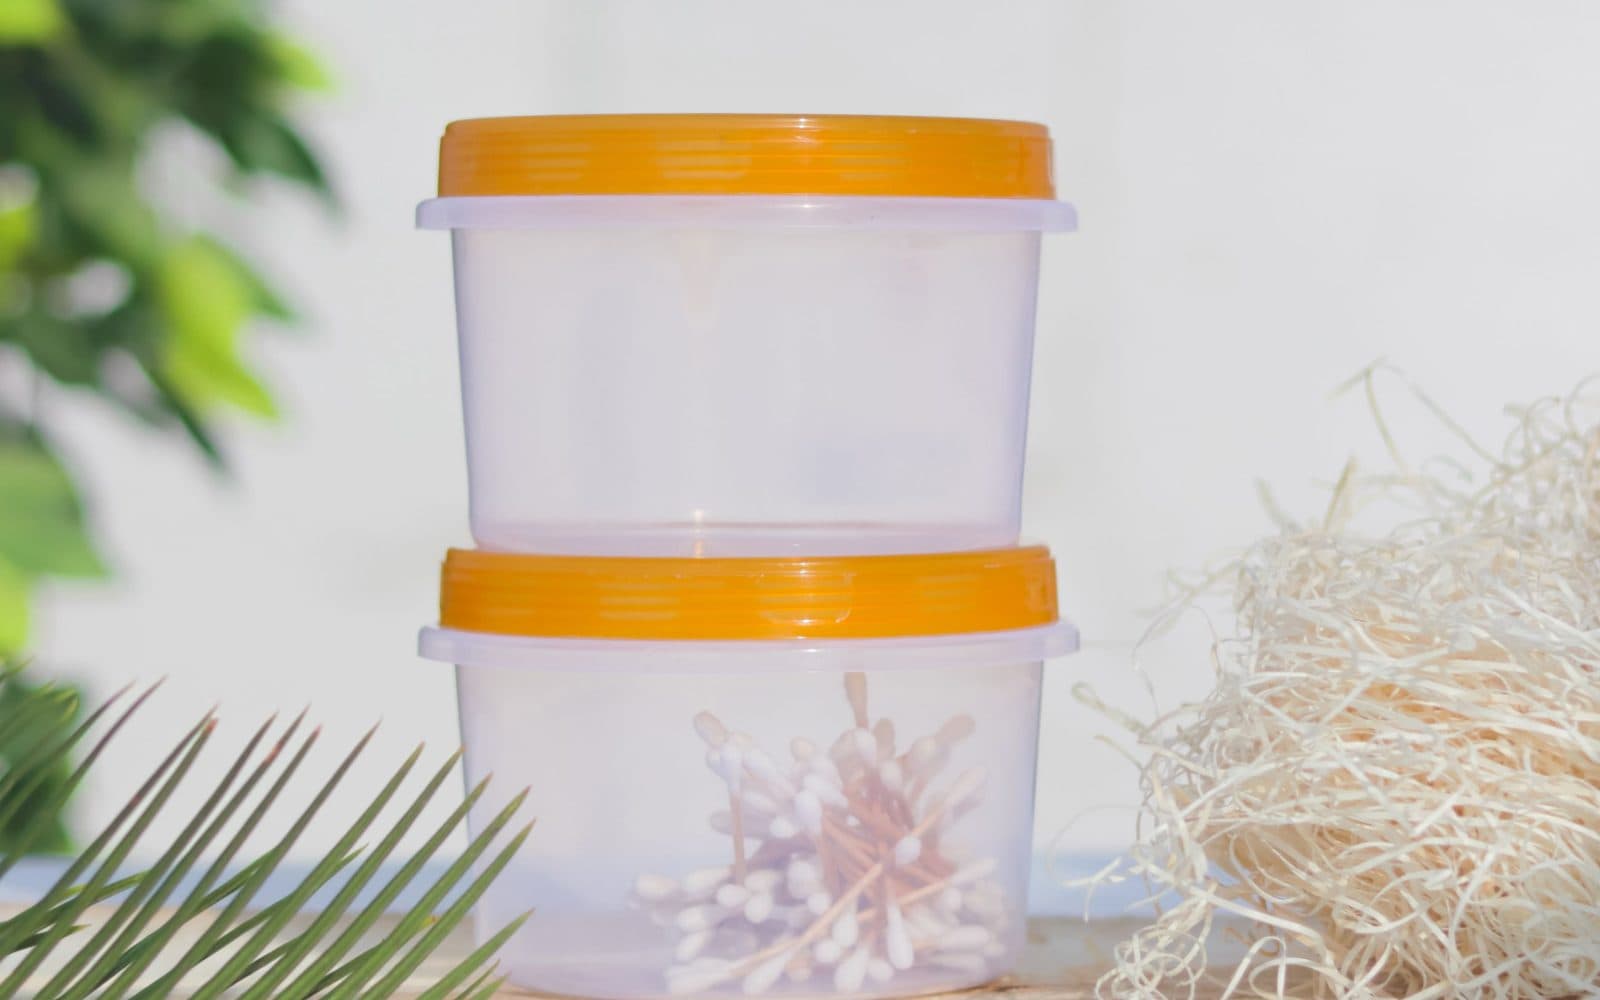
8-cavity 150 g yoghurt tub: cycle 3.1 → 2.6 s
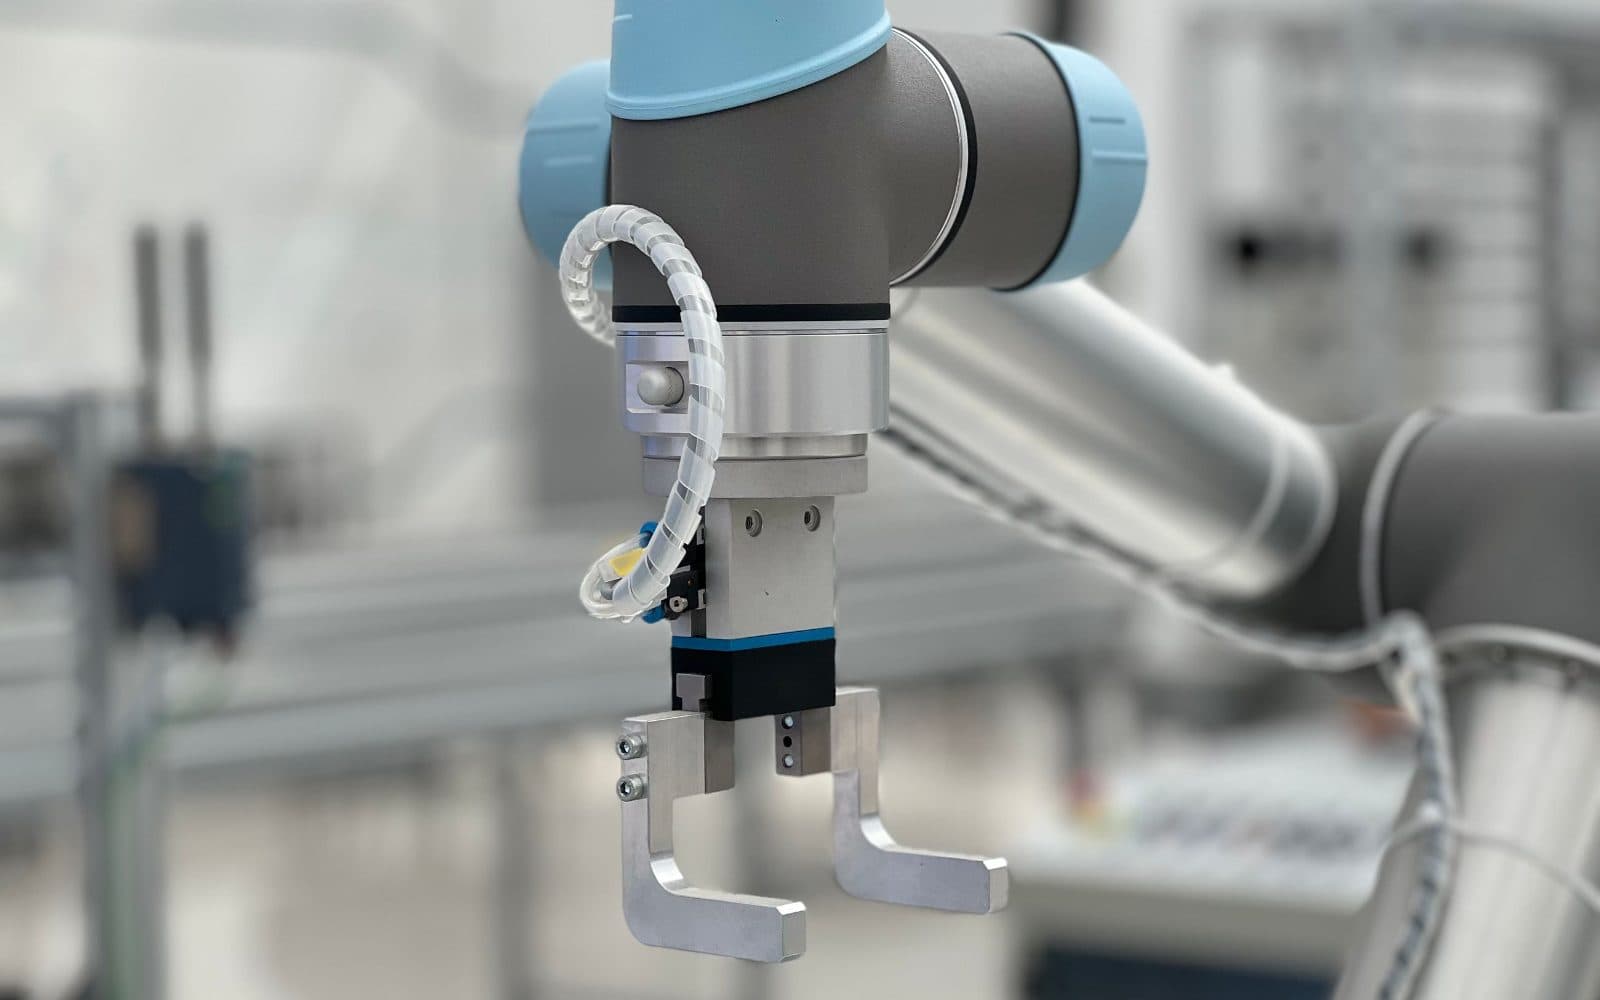
The old top-entry robot on a 380 t machine was replaced with an SE-450; scrap fell from 1.8% to 0.4% and about 1,800 more tubs per hour are produced.
- 3.1 → 2.6sCycle
- 1.8% → 0.4%Scrap
- 45 → 25minChangeover
01Challenge
The customer's 8-cavity 150 g yoghurt tub mould on a 380 t machine ran a 3.1 second cycle with an old top-entry robot; mould intervention reached 1.6 seconds and scrap stood at 1.8% due to double labels and shifting. Two product changes per shift meant 45 minutes of downtime each.
02Solution
An SE-450 side-entry robot was installed with an LM-8 magazine and ES-Charge charging; the EOAT plate was prepared in 5 days with 3D-printed cores to the existing mould dimensions. Recipe-based changeover and motorised guide adjustment brought the switch between the two products down to 25 minutes.
03Result
Cycle fell to 2.6 seconds and intervention to 0.8 seconds; scrap dropped to 0.4%. With about 1,800 extra tubs per hour and 40 minutes less downtime per shift, the investment is expected to pay back in about 14 months.
Result metrics
- 3.1→2.6sCycle
- 1.8%→0.4%Scrap
- 45→25minChangeover
- 9,290→11,080Tubs / hour
Before / After
 BeforeAfter
Drag to compare
Related case studies
Free application analysis
Share your container, label and mould details; we will get back within 48 hours with a cycle and investment projection.